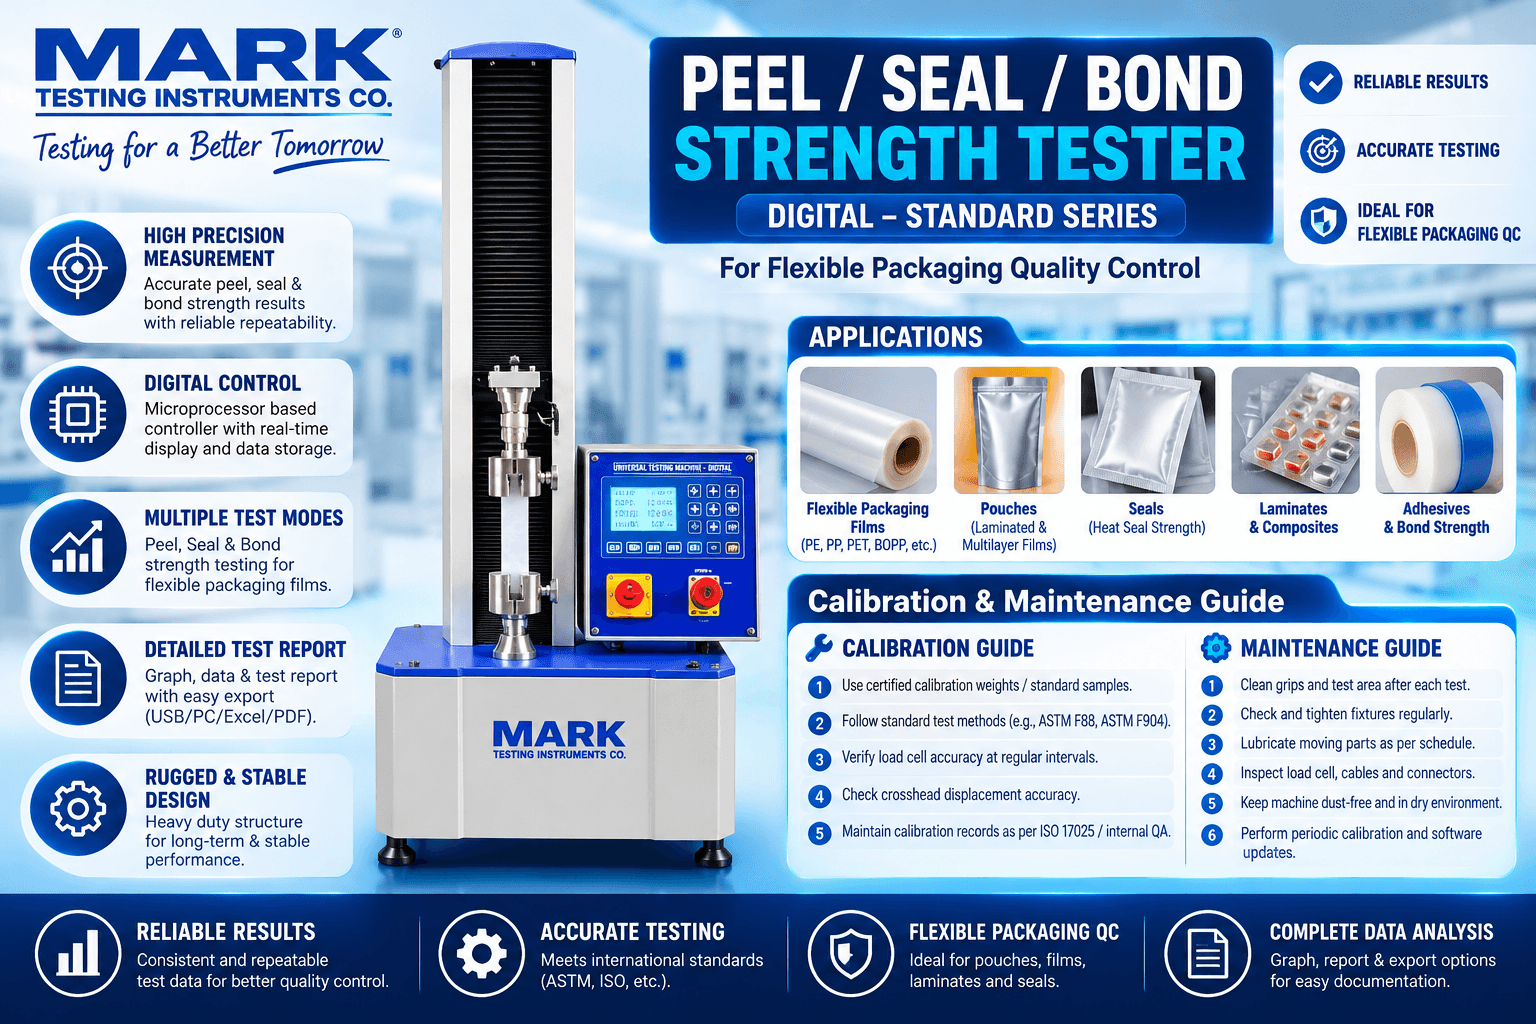
Peel/Seal/Bond Strength Tester Calibration & Maintenance Guide for Reliable QC Results
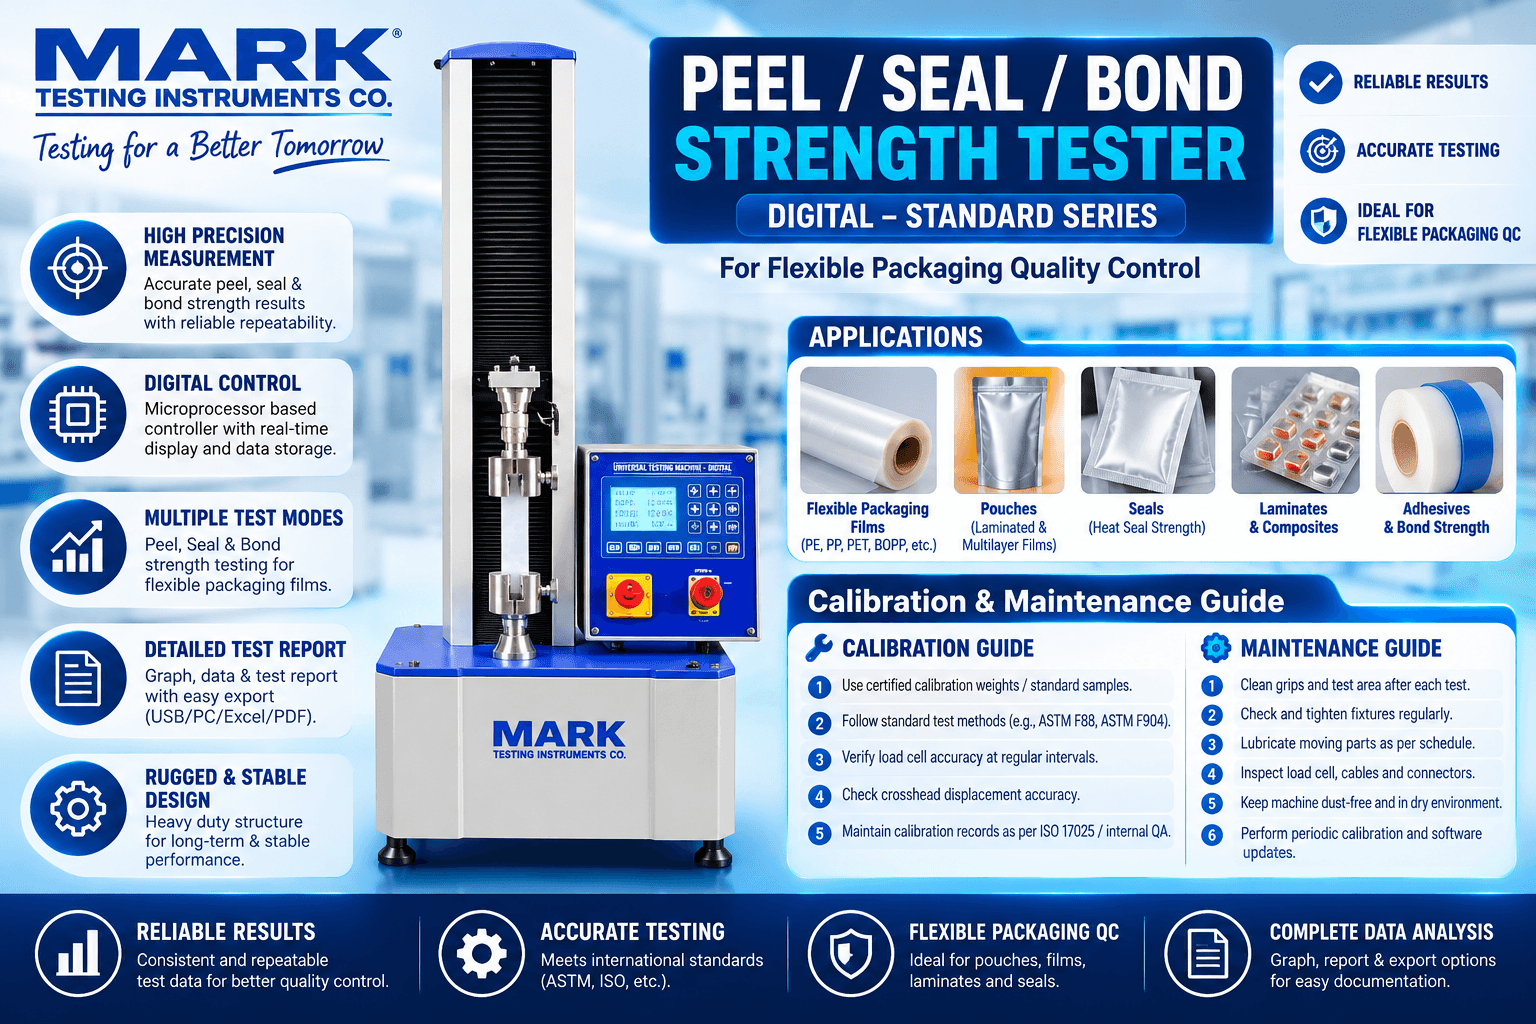
Learn how to calibrate, maintain and inspect a Peel/Seal/Bond Strength Tester for reliable flexible packaging quality control. Covers force verification, grips, test speed, ASTM F88 and ASTM D3330, common errors, preventive maintenance and MARK testing machine configurations.
Peel/Seal/Bond Strength Tester Calibration & Maintenance Guide for Reliable QC Results
A Peel/Seal/Bond Strength Tester is an important quality-control instrument for manufacturers of flexible packaging, laminated films, adhesive tapes, labels and heat-sealed packaging materials.
Reliable test results depend not only on machine accuracy but also on correct specimen preparation, suitable grips, testing speed, calibration and preventive maintenance.
An incorrectly maintained testing machine can produce inconsistent force readings, specimen slippage, inaccurate peel results and unreliable quality-control records.
MARK Testing Instruments offers Digital, Computerized and HMI configurations of Peel/Seal/Bond/Adhesion Strength Testers for flexible packaging and industrial laboratories.
This guide explains the calibration checks, maintenance procedures and testing practices that help laboratories maintain reliable results.
What Is a Peel/Seal/Bond Strength Tester?
A Peel/Seal/Bond Strength Tester is a force-measuring instrument used to evaluate the resistance of suitable materials to separation under controlled loading conditions.
Depending on the fixture and method, it can perform:
- Heat-seal strength testing
- Adhesive tape peel testing
- Laminate peel testing
- Bond strength evaluation
- Adhesion testing
- Suitable 90-degree peel tests
- Suitable 180-degree peel tests
The machine applies controlled movement while measuring the force required to separate the specimen.
The results help manufacturers evaluate packaging seal integrity, adhesive performance and material consistency.
Why Calibration Is Important
Calibration helps establish the relationship between the instrument's measured values and recognized reference values.
For Peel/Seal/Bond Strength Testers, force measurement is particularly important because test results are often reported as force or force per unit specimen width.
Calibration and verification help laboratories:
- Maintain confidence in test results
- Detect measurement drift
- Support repeatable testing
- Identify out-of-tolerance conditions
- Maintain traceable quality-control records
- Meet applicable laboratory quality requirements
Calibration should cover the actual measurement range used by the laboratory.
A machine with a high maximum capacity is not automatically suitable for very low-force testing.
Important Parameters to Calibrate or Verify
1. Force Measurement
Force measurement is the primary parameter.
Check:
- Load-cell performance
- Zero indication
- Force accuracy
- Repeatability
- Relevant working range
- Calibration status
Use suitable calibrated reference equipment and an approved procedure.
2. Crosshead Speed
Peel and seal strength results can depend on the rate of separation.
The testing speed should be verified against the selected test method.
3. Displacement Measurement
Where displacement or extension is reported, verify the measurement system as required by the laboratory procedure.
4. Grip and Fixture Condition
Grips should be inspected for wear, damage and improper alignment.
Fixture condition is an important functional check, although it is not a substitute for instrument calibration.
5. Software Calculations
For Computerized and HMI systems, verify:
- Force units
- Specimen width
- Peak force calculation
- Average force calculation
- Test speed settings
- Report fields
- Result export
Relevant Testing Standards
ASTM F88/F88M — Seal Strength
ASTM F88/F88M addresses seal strength testing of flexible barrier materials.
The procedure and specimen configuration must follow the selected method.
ASTM D3330/D3330M — Peel Adhesion
ASTM D3330/D3330M addresses peel adhesion of pressure-sensitive tape.
The selected procedure must be appropriate for the tape and substrate.
Important Difference
Seal strength and adhesive peel strength are not identical properties.
The same testing frame may support both applications, but specimen preparation, grips, peel geometry and result interpretation can differ.
Step-by-Step Calibration and Verification Workflow
Step 1: Inspect the Machine
Before calibration, inspect:
- Load cell
- Grips
- Crosshead
- Drive mechanism
- Cables
- Display
- Safety switches
- Mechanical frame
Do not use equipment with visible mechanical or electrical damage.
Step 2: Check Zero Indication
Ensure the force measurement system is unloaded and follow the manufacturer's zeroing procedure.
Step 3: Verify Force Measurement
Apply appropriate reference forces using a suitable calibrated system.
Compare the indicated force with the reference values.
Step 4: Check Repeatability
Repeat measurements at selected points according to the approved verification procedure.
Step 5: Verify Test Speed
Check the actual crosshead movement rate against the required speed.
Step 6: Inspect Fixture Alignment
Confirm that grips and fixtures are installed correctly and do not introduce unintended loading.
Step 7: Review Software Results
Where applicable, verify that displayed values, calculations and reports are consistent with the measured data.
Step 8: Document the Results
Record:
- Instrument identification
- Calibration date
- Reference equipment
- Measurement points
- Observed results
- Acceptance criteria
- Calibration status
- Next scheduled review
Step 9: Address Out-of-Tolerance Results
If a parameter falls outside the specified limits, stop relying on the affected measurement function until the issue has been investigated and corrected.
Step 10: Release the Machine for Testing
Resume routine testing only after the instrument meets the laboratory's acceptance requirements.
Daily Maintenance Checklist
Before starting testing:
- Clean the machine and working area.
- Inspect grips and clamping surfaces.
- Check for visible cable damage.
- Verify zero indication.
- Check crosshead movement.
- Confirm test speed settings.
- Inspect the specimen fixture.
- Verify the calibration status.
- Check the emergency stop and safety functions according to the approved procedure.
Weekly Maintenance Checklist
- Inspect grip faces for wear
- Check fixture fastening
- Examine moving components
- Review unusual machine noise
- Check specimen alignment
- Inspect accessible cables and connectors
- Review recent test-result inconsistencies
Periodic Preventive Maintenance
Periodic maintenance should follow the manufacturer's instructions.
Activities may include:
- Mechanical inspection
- Drive-system inspection
- Lubrication where specified
- Load-cell connection inspection
- Fixture inspection
- Speed verification
- Force calibration
- Software and report verification
Maintenance frequency should reflect machine usage, environmental conditions and laboratory quality requirements.
Common Problems and Corrective Actions
Problem 1: Specimen Slippage
Possible causes
- Incorrect grips
- Insufficient clamping
- Worn grip faces
- Improper specimen mounting
Corrective actions
- Use suitable grips
- Adjust clamping
- Inspect grip surfaces
- Prepare a new specimen
Problem 2: Inconsistent Peel Force
Possible causes
- Variation in specimen width
- Incorrect test speed
- Adhesive variability
- Incorrect peel geometry
- Specimen conditioning differences
Corrective actions
- Standardize specimen preparation
- Verify test speed
- Follow the selected standard
- Check fixture alignment
Problem 3: Incorrect Average Peel Force
Possible causes
- Incorrect software calculation region
- Inclusion of unsuitable portions of the force curve
- Incorrect specimen width
- Wrong reporting units
Corrective actions
- Verify the selected calculation interval
- Check dimensions and units
- Review the force curve
- Follow the standard's reporting requirements
Problem 4: Load Reading Does Not Return to Zero
Possible causes
- Residual force
- Mechanical binding
- Incorrect zero procedure
- Measurement-system fault
Corrective actions
- Remove applied force
- Inspect the machine safely
- Repeat the approved zero procedure
- Arrange qualified technical service if required
Problem 5: Irregular Force Curve
Possible causes
- Grip slippage
- Specimen defects
- Vibration
- Incorrect fixture geometry
- Measurement noise
Corrective actions
- Inspect specimen mounting
- Verify grips
- Check test conditions
- Review machine performance
MARK Peel/Seal/Bond Strength Tester Configurations
Digital — Standard Series
Suitable for routine peel, seal and bond force measurement.
Selected specifications include:
- Load-cell options: 3 kgf and 10 kgf
- Readability: 0.001 kg
- Stated accuracy: ±0.05%
- Digital load indication
- Peak-hold function
- Variable-speed operation
Digital with Printer
Provides digital force measurement with printed result documentation on the configured model.
Computerized — Smart Series
Designed for software-based test control and reporting.
Depending on configuration, features can include:
- Real-time force graph
- Peak force
- Average force calculations
- Electronic test records
- Report generation
- Data export
HMI Touchscreen
Designed for standalone touchscreen operation with test settings and result management.
HMI-cum-Computerized
Combines touchscreen operation with computer-based functionality on the specified configuration.
Technical Specifications to Confirm
| Parameter | Specification |
|---|---|
| Instrument | Peel/Seal/Bond/Adhesion Strength Tester |
| Brand | MARK Testing Instruments |
| Standard Digital Load Cells | 3 kgf / 10 kgf |
| Digital Readability | 0.001 kg |
| Stated Digital Accuracy | ±0.05% |
| Speed | Variable, model dependent |
| Test Geometry | According to fixture and method |
| Peak Hold | Available on Digital model |
| Printer | Selected configurations |
| Computer Software | Selected configurations |
| HMI | Selected configurations |
| Warranty | 12 Months |
Final specifications and the basis of the stated accuracy should be confirmed in the model quotation.
How Often Should the Tester Be Calibrated?
There is no universal calibration interval suitable for every machine.
The laboratory should determine the interval based on:
- Frequency of use
- Previous calibration results
- Required measurement accuracy
- Instrument stability
- Customer requirements
- Laboratory quality procedures
- Applicable accreditation requirements
An annual calibration interval is commonly considered by laboratories, but the actual schedule should be justified by the laboratory's requirements.
Peel/Seal/Bond Strength Tester Price and Maintenance Cost in India
Equipment and maintenance costs depend on:
- Load capacity
- Load-cell configuration
- Controller type
- Software
- Printer
- HMI touchscreen
- Test fixtures
- Calibration scope
- Installation requirements
- Spare parts
- Preventive maintenance needs
A suitable machine should be evaluated on both purchase price and long-term measurement reliability.
Frequently Asked Questions
What is the difference between calibration and maintenance?
Calibration evaluates measurement performance against reference values. Maintenance involves inspecting and servicing the equipment to keep it functioning correctly.
Which standard is used for heat-seal strength?
ASTM F88/F88M is a relevant method for seal strength of flexible barrier materials.
Which standard is used for adhesive tape peel testing?
ASTM D3330/D3330M is relevant to peel adhesion of pressure-sensitive tape.
Can one machine perform peel, seal and bond testing?
Yes, a suitably configured testing machine can support multiple methods using the appropriate grips, fixtures and test settings.
Is a Computerized model available?
Yes. MARK offers Computerized Peel/Seal/Bond Strength Tester configurations.
Is an HMI model available?
Yes. MARK offers HMI configurations with features dependent on the selected model.
Request a Peel/Seal/Bond Strength Tester Quotation
MARK Testing Instruments offers Digital, Printer, Computerized and HMI configurations for flexible packaging and adhesive testing laboratories.
For technical selection, provide:
Material + Test Standard + Expected Force + Specimen Width + Peel Geometry + Reporting Requirements
MARK Testing Instruments
Email: sales@marktestinginstruments.com
Website: www.marktestinginstruments.com